A process capability index is meaningful only after the bag characteristic, tolerance, measurement method, production conditions, sampling order, and statistical model are defined. A high Cpk from a short hand-selected run does not prove stable production. First verify the measurement system and time behavior; then calculate and interpret capability.
Machine Accuracy and Process Capability Are Different Questions
Machine accuracy asks whether a controlled mechanism can reach a commanded position under stated conditions. Process capability asks how the complete production result varies relative to a product specification. PP nonwoven behavior, roll winding, tension, print repeat, tooling, speed, operator setup, temperature, and measurement all contribute to finished bag dimensions.
A Supplier may demonstrate a stable feed mechanism, while the final gusset still varies because the web folds differently across material lots. Keep mechanism tests and finished-product capability studies separate.
Define the Characteristic Without Ambiguity
Bag length sounds simple until one inspector flattens the bag, another includes a fold, and a third pulls the flexible fabric taut. The specification should include datum, measurement path, specimen state, applied flattening or force, instrument, resolution, environmental conditioning if required, and upper and lower limits.
| Characteristic | Definition detail needed | Likely variation source |
|---|---|---|
| Bag length | Cut edge to datum, relaxed or flattened state | Feed slip, tension, encoder scaling, cut timing |
| Bag width | Flat body or including gusset | Web width, folding, lateral position |
| Gusset depth | One side or total opened depth | Former position, layer drag, operator setup |
| Handle position | Centerline to bag datum | Feed synchronization, tooling, bag tracking |
| Print-to-cut position | Artwork datum and direction | Print repeat, photo-eye, web stretch |
Prove the Measurement Process Before Studying the Line
If two inspectors measure the same flexible bag differently, process indices mix production variation with measurement variation. Check instrument resolution, calibration status, fixture, method, repeatability, operator reproducibility, sample handling, and rounding.
ISO 22514-7 addresses capability of measurement processes and explains why measurement uncertainty must be adequately small before capability or performance indices are meaningful. Use the current licensed edition and qualified statistical support for formal studies.
Design a Study That Includes Time
Twenty consecutive bags after an expert adjustment describe a short moment. They do not include roll-diameter change, warm-up, normal stops, operator intervention, splice passage, or material variation. Sample in production order and retain the time sequence.
- Identify machine, serial number, tooling, software, and recipe.
- Record fabric Supplier, lot, roll, width, GSM, and print condition.
- Include defined low, normal, and high operating states where commercially relevant.
- Sample across the run rather than selecting attractive bags later.
- Mark adjustments, stops, roll changes, alarms, and maintenance on the data plot.
- Keep product families separate unless a justified model combines them.
Look at the Plot Before Cp or Cpk
Plot measurements in production order. Check for trends, cycles, shifts, outliers, mixtures, and changes in spread. A distribution made from two different recipes may look wide even though each recipe is internally consistent. A steady drift with roll diameter points to a different problem than random variation.
| Pattern | What an index may hide | Next action |
|---|---|---|
| Stable center and spread | Possible normal process behavior | Evaluate distribution and capability |
| Mean shifts after adjustment | Two process states averaged together | Separate states and control adjustment |
| Progressive drift | Time-dependent loss of centering | Investigate roll, heat, tension, wear, or control |
| Cyclic variation | Mechanical rotation or repeated process event | Compare period with roller, drive, or tooling cycle |
| Rare large outliers | Special causes diluted in the standard deviation | Trace the exact timestamp and event |
Interpret Capability and Performance with the Right Model
Cp commonly compares potential spread with a two-sided tolerance when the process is stable and the model assumptions apply. Cpk also reflects off-center operation. Performance indices such as Pp and Ppk are often calculated using longer-term variation. Names and formulas should follow the organization’s chosen standard and software.
ISO 22514-2:2026 covers capability and performance statistics for time-dependent process models and recognizes different distribution types. Do not force non-normal, mixed, or unstable data into a normal-distribution formula merely because the software offers Cpk.
A Capability Number Does Not Replace Defect Control
Capability describes a measured characteristic under the study conditions. It does not validate seam strength, handle function, print adhesion, contamination, or safety. A centered bag length can coexist with weak welding. Maintain separate control plans for attribute defects and functional tests.
Also preserve the raw data. A buyer should be able to see sampling order, excluded points, reason for exclusion, measurement-system status, statistical model, and software settings. Reporting only Cpk prevents an independent review.
Use Capability in FAT and Improvement Without Gaming It
Before FAT, agree on product, material, tolerance, study duration, sample plan, speed, allowed adjustments, measurement method, and index interpretation. State whether the study measures a short-term machine condition or a broader production process. Do not change limits after seeing the data.
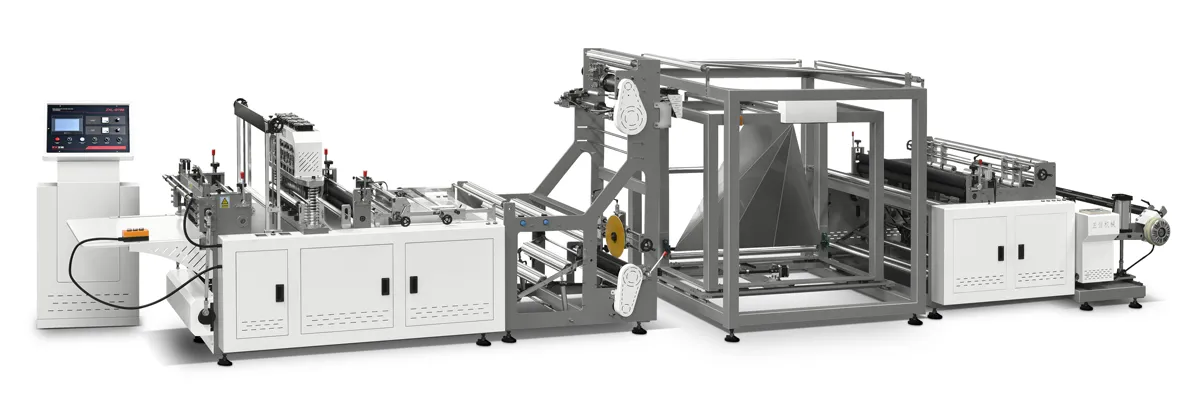
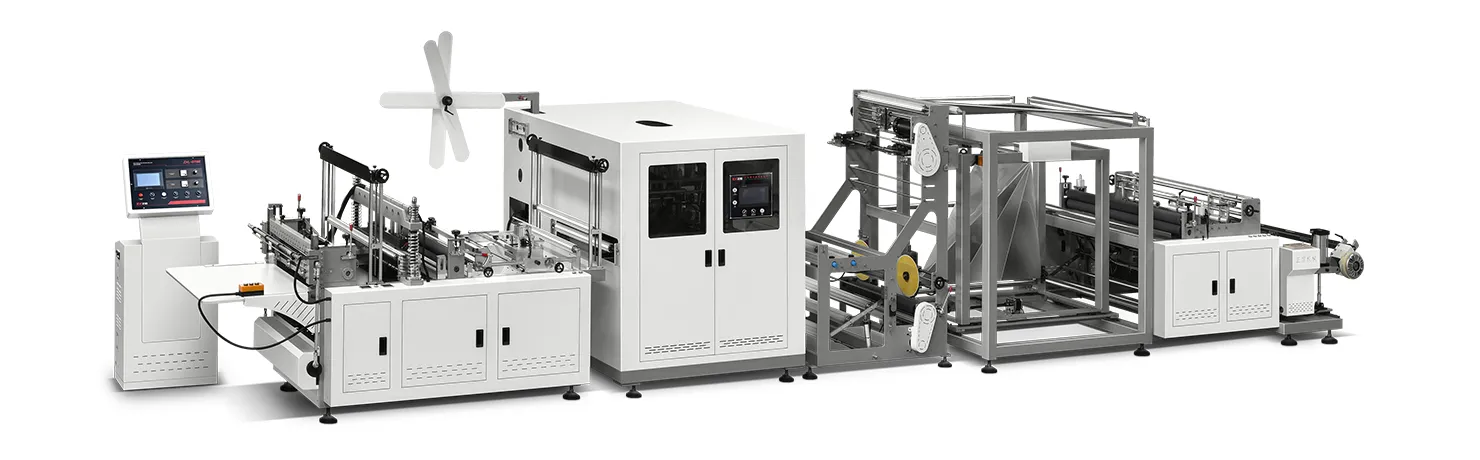
Send Zhengxin your bag drawing, measurement method, ordered data, material and recipe identity, speed history, and adjustment log. We can help map variation to the feed, web, folding, tracking, handle, ultrasonic, or cutting system of the delivered Manufacturer configuration. Formal statistical acceptance should be reviewed by the buyer’s quality specialist.
 አማርኛ
 English
 العربية
 Español
 Русский
 O‘zbekcha
 Қазақ тілі
 Português (AO90)
 Tiếng Việt
 (فارسی (افغانستان
 Kiswahili
 தமிழ்
 Bahasa Indonesia
 اردو
 हिन्दी
 বাংলা