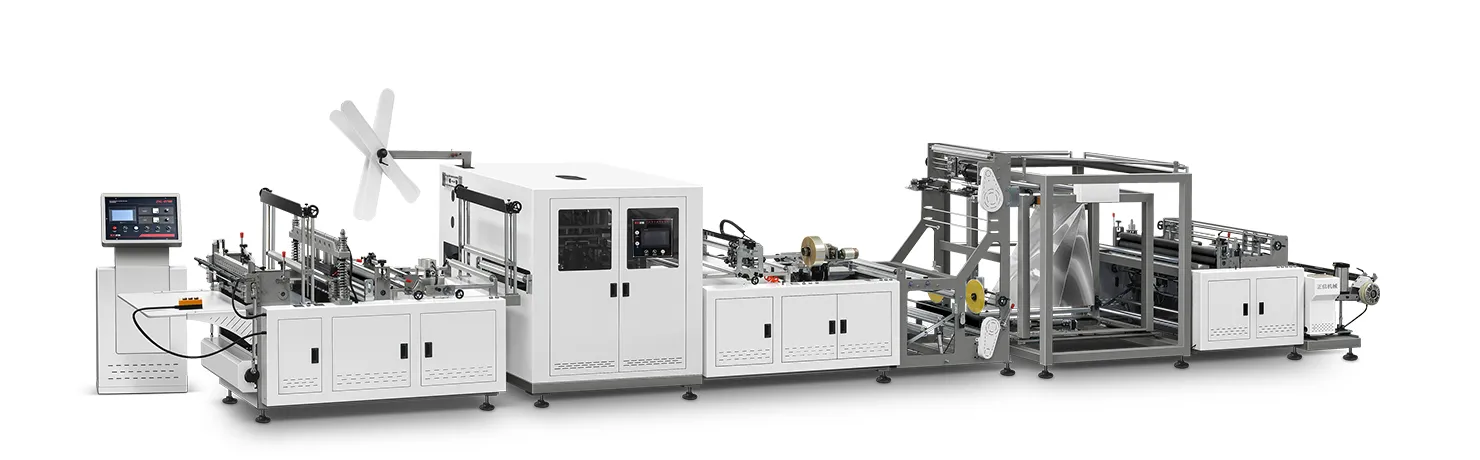
A D-cut handle is not a cosmetic detail. It is a load-bearing opening, a touch point for the customer, and a fast visual signal of whether a bag was made under control. The practical objective is not to run a punch until it visibly fails. It is to recognize a changing edge before it creates an avoidable cluster of rejects, handle tears, customer complaints, or an unplanned stop.
This guide is written for a buyer, production manager, maintenance lead, or quality engineer working with PP non-woven bag converting. It explains how to separate tool-condition evidence from fabric variation, web tension, registration, stack alignment, and inspection bias. It does not prescribe a universal punch life. Die geometry, fabric basis weight, laminations, handle size, speed, reinforcement, heat, maintenance method, and machine design all change the answer. Use the approved machine manual, the validated bag specification, and a qualified technician for machine-specific work.
Start with the customer-visible failure, not a generic maintenance interval
“The handle edge looks bad” is too vague to control. Turn the complaint into an observable defect family. A fuzzy perimeter, a partially severed fibre bridge, an asymmetric D shape, a crushed edge, a torn corner, a shifted opening, and a handle that tears when pulled can appear at the same time, but they do not point to the same first cause. A fixed replacement interval alone therefore creates two expensive mistakes: replacing a still-capable tool early, or continuing to run a degrading tool because the calendar has not reached its date.
Begin by agreeing on the exact product definition. Record the bag style, fabric construction, basis weight and tolerance where available, coating or lamination, handle artwork position, nominal opening dimensions, acceptable edge appearance, destructive-test method if one is used, and the sampling rule. Photograph a conforming approved sample from both sides in consistent lighting. That sample is more useful than a verbal standard such as “clean cut,” because it gives operators, suppliers, and buyers a shared visual reference.
The usual mistake is to inspect only the opening after the punch. Instead, inspect the sequence around it: incoming fabric, web path, print mark or length registration, cut position, stacking, and finished-bag handling. A dull or damaged punch can create roughness. So can tension that pulls fibres during severing, a drifting web, contamination on a support surface, uneven clamping, or a measurement method that changes from one inspector to the next. The purpose of diagnosis is to reject competing explanations with evidence, not to attach a plausible label to the first bad bag.
Build a defect language that operators can use consistently
| Observed condition | What it may indicate | First evidence to collect |
|---|---|---|
| Even, fuzzy edge around the full D-cut | Progressive tool condition change, material response, or insufficiently clean severing | Time-ordered samples, tool-face inspection, fabric-lot comparison |
| One rough zone at the radius or shoulder | Local nick, alignment issue, support/anvil condition, or local contamination | Map the defect to tool orientation and inspect the same location |
| Fibres remain attached intermittently | Incomplete cut, changing material, pressure/energy inconsistency, or debris | Sample rate by speed, line position, lot, and accumulated stroke count |
| D-cut is shifted from artwork or panel | Registration, web tracking, recipe, sensor, or feed issue rather than punch wear | Compare opening position and repeat-mark position separately |
| Crushed or glossy border | Excess force, dwell, support surface, heat, or material finish interaction | Inspect both faces, log settings, and compare with a known-good run |
| Handle tears in use or pull testing | Geometry, reinforcement, fabric properties, seam proximity, or edge damage | Document failure origin, test setup, and sample conditioning |
Make the language visual. Place a one-page defect board near the line with named photographs, severity examples, and the action allowed at each level. For example, an operator may be allowed to clean a specified accessible surface using an approved method, but not to change a guarded tool, alter a force setting, or improvise a sharpening method. A technician may be allowed to inspect or replace the tool under the documented energy-control procedure. A quality lead may decide whether an observed condition is a process alert, a hold trigger, or acceptable variation. Clear authority reduces both delayed escalation and well-meant unapproved adjustments.
Why a single stroke count is useful but insufficient
Stroke count belongs in the record because it gives maintenance a common clock. It does not prove the same amount of wear has occurred. A run of lightweight uncoated fabric at moderate speed may load the cutting system differently from a short urgent order with a laminate, darker print, more dust, frequent stops, or a tighter edge-appearance expectation. A machine may also experience events that do not show up in the stroke total: a folded web, a foreign particle, a support-surface mark, a tool contact incident, or an incorrect setup.
Use stroke count as one axis of a condition model, alongside product family, fabric supplier/lot, speed band, setting revision, number of stops, cleaning history, observed defect score, and inspection result. The model can start simply in a spreadsheet. Its purpose is not predictive maintenance theatre. It is to make a maintenance decision auditable: “We inspected this tool after this production exposure, under this product family, and found this condition.” When the same evidence is collected over several cycles, the factory can identify a practical inspection window for its own approved combination of machine, tool, and material.
Toolmakers in other punching applications similarly emphasize that maintenance discipline supports precise, high-quality punching. TRUMPF’s tooling guidance makes that point for its own punching context. Its catalogue describes tool maintenance as important to long life and precise, high-quality punching. That is not evidence that a PP non-woven D-cut tool has the same wear mechanism as a sheet-metal punch. It is a transferable management principle: inspect condition, preserve the evidence, and validate the result on the actual material and tool system.
Create an inspection route before adjusting a process setting
A reliable route moves from the least invasive observations to the most invasive checks. First, preserve the run conditions. Mark sample order, do not mix suspect bags into a stack, and note whether the problem appeared at startup, after a roll splice, after a speed change, or late in a run. Confirm the actual recipe name and revision. Record target speed, actual speed, material lot, operator shift, accumulated strokes, and any alarm or stop. If the product is printed, keep the evidence needed to compare the print-to-opening position.
Second, inspect what can be checked without entering a hazardous zone: fabric roll condition, web folds, dust, residue, scraps, support-surface cleanliness, stack condition, and visible output consistency. Third, after the documented shutdown and energy-isolation procedure, have authorized personnel inspect the punch, mating surface, mount, fasteners, alignment references, and surrounding guides according to the OEM instructions. Never use a hand near a tool zone merely because a line appears stopped. A stopped drive, stored pneumatic energy, gravity, automatic restart logic, or another energy source can still create risk.
Fourth, establish whether the defect travels with the tool. If the same rough point appears at the same clock position around the D-cut across a sequence of bags, that supports a localized tool or support hypothesis. If the roughness moves with print position, roll width, or tension changes, the tool may be innocent. This “fixed orientation versus moving orientation” question is simple and powerful. It prevents a factory from replacing a tool while the true cause remains in web control.
Separate edge appearance from opening location
Two different control loops are often mixed together. Edge quality asks whether the material was cut or formed cleanly. Opening location asks whether the D-cut was created in the correct place relative to the bag panel, print, and reinforcement. An article about punch wear becomes misleading if it treats every handle complaint as a tool problem.
Measure location with a defined datum. For a printed bag, choose a stable print feature or a physical bag edge specified in the drawing. For an unprinted bag, use a stable panel datum. Measure the opening centre, left/right shoulder, and top/bottom relation as relevant to the customer drawing. Then inspect the edge independently with a visual standard and, where justified, a destructive or functional test. A shifted but clean opening is primarily a registration or feed investigation. A correctly located but ragged opening is more likely to need a condition, material, or cutting-process investigation. Both conditions together can have two simultaneous causes.
Do not let sampling hide a pattern. A final inspection of five randomly pulled bags can miss a defect that appears every time a particular roller orientation, splice, or tool location occurs. During diagnosis, take a sequence: for example, consecutive numbered samples at a defined interval through a controlled run. The number and interval should be selected from the defect frequency and order risk, not copied blindly from another factory. Keep the time order intact so an engineer can compare defect onset with speed, roll, and events.
Control the material and web conditions that can imitate wear
PP non-woven fabric is not a perfectly uniform rigid substrate. Fibre arrangement, basis-weight variation, surface treatment, laminate, humidity and storage condition, print coverage, static, web tension, and fold condition can change how an opening looks. A buyer should not accept “material issue” as an unsupported conclusion, but neither should a factory treat every fibre bridge as proof that tooling needs replacement. Require a side-by-side trial using the same approved tool and settings, with material lots clearly identified. If the edge quality changes by lot while the tool and machine evidence remain stable, material becomes a stronger branch of the investigation.
Incoming checks do not need to become a laboratory project. Define the few properties that matter to the final D-cut: correct style and width, visible surface uniformity, roll damage, treatment or lamination status when specified, and traceable lot identity. Where a customer specification calls for a tensile or other test, document the method, conditioning, direction, sampling, and acceptance rule. ISO 9073-3 covers tensile-strength and elongation determination for nonwovens; the ISO landing page identifies the method’s scope. It does not replace a bag-handle acceptance method, and it should not be cited as if it proves a particular finished-bag load rating.
Web tension deserves its own record because it can alter the way a cut opens, stretches, or registers. Look for dancer position trends, unwind braking changes, edge wandering, wrinkles before the handle station, roll splice location, and speed transitions. A tension correction made during a fault should be recorded as an event. Otherwise, later comparison becomes impossible: the team may conclude a tool replacement fixed the edge when a tension change was the true improvement.
Use a controlled change plan instead of “turning knobs until it looks better”
When a defect is active, production pressure encourages simultaneous changes: lower speed, change pressure, clean the surface, tighten a guide, alter a sensor, and replace the tool. The output may improve, but no one knows why. That uncertainty returns on the next order and becomes a cost hidden in scrap, setup time, and buyer confidence.
Design a compact controlled trial. Freeze the recipe backup and capture the pre-change state. Select one primary hypothesis. Change one factor that is authorized and safe to change. Run a defined number of sequential bags at a documented speed and material condition. Measure the same dimensions using the same method. Record edge severity, location, fibre bridges, reject count, and any secondary issue. Return to the approved setting only if the change creates an unacceptable effect. If the first test does not discriminate between hypotheses, decide what evidence would: a tool rotation check, alternate material lot, different speed band, or authorized replacement comparison.
Do not make general statements such as “more pressure makes a cleaner cut.” Process settings interact with tooling, material, and equipment design; an increase that improves one appearance issue can create crushing, premature wear, or a safety and reliability problem elsewhere. The right conclusion is conditional: “Under the approved setup, this authorized change produced this measured result on this material lot.” That conclusion is useful to the next shift and honest to the buyer.
A practical evidence sheet for each tool event
| Field | Why it matters | Example of useful entry |
|---|---|---|
| Tool ID and orientation | Links observations to an actual physical item | D-cut tool DC-04; reference mark at 12 o’clock |
| Machine and station | Separates tool behavior from line-to-line conditions | Line B; handle opening station 2 |
| Product/recipe revision | Prevents comparing different requirements as one population | Bag family, opening drawing revision, approved recipe ID |
| Material identity | Allows lot-based analysis and supplier follow-up | Fabric supplier, roll ID, incoming inspection reference |
| Production exposure | Creates a condition-history axis | Stroke counter start/end and stop events |
| Observed evidence | Makes a replacement decision explainable | Photo scale, defect code, location, sample sequence |
| Action and authority | Prevents untraceable changes | Cleaned by authorized technician; replacement approved by maintenance lead |
| Validation result | Closes the loop rather than assuming success | Defined samples passed appearance/location review at agreed speed |
Photographs should include a scale, product or sample identifier, and orientation. A close-up without context is often unusable later. Take one wide image showing the whole opening and one close image of the defect; avoid retouching. Retain the physical samples when the order value, complaint risk, or investigation warrants it. The same evidence package can support internal maintenance, a fabric supplier claim, an OEM/ODM service discussion, or a buyer’s corrective-action request.
Set alert limits before a customer sees the trend
A mature process does not wait for a pass/fail cliff. It creates an alert band. For edge appearance, the band may be a defined count of fibre bridges per opening, a visual defect grade against an approved panel, a trend in functional-test failure, or a rise in rework rate. For location, it may be a measured deviation trend. The exact limits must come from the buyer-approved specification and realistic process capability, not an arbitrary number in a generic blog.
Make the escalation response specific. An alert may trigger increased sequential sampling and technician inspection; a hold limit may stop packing of affected bags and preserve traceability. The response should name who decides, which lots are affected, what evidence must be saved, and when a buyer is informed. This is also how a manufacturer demonstrates credible control during supplier qualification: not by promising zero defects, but by showing how a small signal is detected, contained, investigated, and verified.
For customized or OEM equipment, agree which data are available from the control system and which must be collected manually. A stroke counter, recipe history, alarm log, and documented photo process are often more valuable than a sophisticated dashboard with no common definitions. Any remote-support discussion should start from the same package: machine serial number, tool ID, product/recipe, material lot, sample order, photos, and the exact symptom. That reduces unnecessary parameter changes and speeds a responsible technical response.
Case study direction: prove whether condition monitoring reduces edge-related loss
This is a study design, not a reported Zhengxin customer case. A factory that wants credible evidence can run a before-and-after study over comparable production families. In the baseline period, retain the existing maintenance approach but collect the evidence sheet for every D-cut-related defect, tool event, scrap disposition, and unplanned stoppage. In the trial period, introduce the agreed inspection trigger and visual defect board, without changing unrelated product specifications. Separate results by fabric family, bag design, and speed band; otherwise a favorable mix change can be mistaken for improvement.
The primary measures could be edge-related reject rate per defined output, number of stops attributed to the station, mean time from alert to authorized decision, and rate of defects detected before packing. Secondary measures could include tool-change duration, rework, and buyer complaint rate, but only if definitions and exposure are consistent. Record both positive and negative findings. If inspections increase planned maintenance minutes while reducing unplanned interruptions, report both; the business decision depends on the whole pattern, not a selectively chosen metric.
A good study also tests whether inspectors agree. Give multiple inspectors the same blinded sample set and compare the defect code they choose. If agreement is poor, the apparent process trend may be a scoring problem. Improve the visual standard before drawing a conclusion about tooling. Keep original photos, raw counts, exclusions, and the method for identifying comparable lots. That documentation makes an internal case study credible enough to inform a buyer discussion without exaggerating what was proved.
What an overseas buyer should ask a Chinese manufacturer
The most useful question is not “How many bags can the machine make per minute?” Ask how handle-opening quality is defined, monitored, and released for the product you intend to buy. Ask to see an approved sample, dimensional datum, edge appearance standard, traceability method, and corrective-action flow. If a custom bag or Customizable machine configuration is under discussion, ask which elements will be confirmed during sample approval: tool geometry, fabric range, reinforcement layout, register relationship, line speed band, inspection method, and spares.
Ask how the supplier distinguishes a tool issue from a material or registration issue. Ask whether tool IDs and maintenance records are retained, whether retained samples are available, and what data would be needed for remote technical support. The answer does not have to be a complicated software system. It should demonstrate a disciplined sequence: contain the affected product, preserve evidence, test a hypothesis, validate the correction, and update the approved setup where justified.
Finally, align contractual wording with what can actually be verified. A blanket promise of “perfect handles” is less useful than a mutually approved inspection criterion, AQL or sampling plan where applicable, packaging and lot definition, response timeline, and evidence package. The buyer gains a repeatable basis for acceptance; the Supplier gains a clear specification instead of subjective late-stage inspection.
Implement the system in four practical stages
- Week one: define. Gather approved samples, drawings, current complaints, tool IDs, and existing records. Create the defect language and authority matrix.
- Weeks two and three: observe. Collect time-ordered samples and event records without changing everything at once. Identify the largest unknowns.
- Weeks four and five: test. Run authorized, safe comparisons that discriminate between tool, material, tension, and registration hypotheses.
- Then standardize. Set inspection triggers, alert actions, training, spare planning, and a periodic review of the actual evidence.
Do not confuse standardization with rigidity. Update the plan when a new bag construction, fabric supplier, tool revision, or machine configuration changes the risk. Preserve the old and new version so an auditor or buyer can understand when the control changed and why. The goal is a living manufacturing record that makes a clean D-cut repeatable, not a binder that is opened only when a complaint arrives.
Make release decisions with evidence that survives a handover
Release is the point where production information becomes a commercial promise. A bag can be physically packed and still be poorly documented. When the line reports a suspected handle issue, identify the last confirmed good sample, the first suspect sample, the last suspect sample, and the first confirmed recovered sample. Tie those boundaries to the finished-bag lot, carton or pallet identification, and production time. If the exact boundary cannot be demonstrated, treat the affected scope conservatively until it is resolved. This protects the buyer and stops the factory from spending days later trying to reconstruct a mixed stack from memory.
Use a disposition vocabulary that tells the next person what happened: accepted under normal release; held pending review; reworked under approved instruction; scrapped; released after documented additional inspection; or returned to a prior stage. Avoid ambiguous terms such as “checked” or “handled.” A check is not a result unless it records what was checked, by whom, with which method, against which acceptance rule, and what decision followed. The record should also say whether an approved recipe, tool, or material changed after the event.
For export orders, the document package must be intelligible to people who did not stand beside the machine. Use unambiguous English names, date/time convention, machine and product identifiers, and photographs that show the same orientation as the drawing. If the buyer uses its own quality template, map your factory data fields to it before mass production. This avoids a common failure at pre-shipment inspection: the factory has useful evidence, but the buyer cannot link it to the lot being inspected.
Train for diagnosis, not only for an acceptable-looking sample
New operators can learn to compare a bag with a reference quickly, but a robust line also teaches them how to communicate a trend. Training should cover the defect families, the correct sample labeling method, where to find the current approved sample, how to recognize a condition that requires an immediate stop or escalation, and which actions are prohibited. Ask operators to explain the difference between a fixed-orientation defect and a travelling defect. That single question reveals whether the team understands why evidence order matters.
Run short challenge exercises using retained nonconforming samples or annotated images. Give each group a simulated sequence: perhaps a rough corner beginning after a material splice, a clean but shifting opening, and a bag with a local tear near a reinforcement. Ask them to choose the first evidence to capture rather than the first adjustment to make. Review the answers against the authority matrix. The point is not to create a test score; it is to reduce the delay between a weak signal and a useful technical record.
Maintenance and quality personnel need a second layer of training: safe access requirements, tool identification, condition photography, inspection method, limits of their authority, and the difference between replacing a component and proving the outcome. The most effective training materials are often the factory’s own real examples, stripped of customer-sensitive information. Each confirmed investigation can add one more photo and one more “what changed the conclusion” note to the visual standard.
Use a simple decision tree during a live fault
First ask whether the defect creates an immediate safety, customer, or containment risk. If yes, follow the documented stop and lot-control process. If not, preserve a consecutive sample sequence and determine whether location and edge quality are both affected. When location is wrong but the edge is clean, verify registration, web feed, and recipe before requesting a tool change. When the edge defect has a fixed tool orientation, make authorized safe inspection of the tool and mating surface a priority. When the defect follows a fabric roll or speed change, compare controlled material or operating conditions before deciding that wear is the principal cause.
After any intervention, repeat the original observation rather than declaring success from one attractive sample. A validated correction has a defined run condition, a defined number of samples, a documented inspection method, and a clear decision. If the fault cannot be reproduced, record that uncertainty. An honest open finding is safer than a confident but unsupported root cause. Escalate to the Manufacturer or technical Supplier with the evidence pack when the condition lies outside local authority, involves a guarded mechanism, repeats after approved action, or threatens a buyer commitment.
Frequently Asked Questions
How often should a D-cut punch be replaced?
There is no responsible universal interval. Use the actual bag design, fabric family, approved settings, accumulated exposure, inspection evidence, and functional/appearance requirement to establish a local trigger. Replace or service the tool through the documented OEM procedure when evidence and authorized inspection support that decision.
Does a rough handle edge always mean the punch is dull?
No. A rough edge can also be associated with material variation, contamination, web tension, support-surface condition, alignment, registration events, or an unsuitable process condition. Compare defect orientation, time sequence, tool evidence, and material lots before assigning a cause.
Can we improve the edge simply by increasing speed or pressure?
Do not assume so. Settings interact with the specific machine, tool, and material. Use only authorized adjustments, record one controlled change at a time, and validate the finished opening against the approved specification. Never bypass guarding or safety controls to speed a trial.
What information should be sent to the machine supplier when an edge-quality problem occurs?
Send the machine serial number, tool ID, product and recipe revision, fabric roll/lot identity, ordered sample photos with scale, dimensions, speed, stroke history, alarm/stop history, and a concise description of when the defect began. This is far more actionable than a single close-up image.
How can a buyer include handle-edge quality in pre-shipment inspection?
Agree the visual standard, dimensional datum, sampling plan, product-lot definition, escalation rule, and photo/retained-sample process before production. For critical bags, also agree the functional-test method, conditioning, and acceptance rule. These details make inspection repeatable across languages and locations.

 አማርኛ
 English
 العربية
 Español
 Русский
 O‘zbekcha
 Қазақ тілі
 Português (AO90)
 Tiếng Việt
 (فارسی (افغانستان
 Kiswahili
 தமிழ்
 Bahasa Indonesia
 اردو
 हिन्दी
 বাংলা