
OEE is useful on a non-woven bag line only when time, speed, total count, good count, and scrap are measured at the same production boundary. The first job is not calculating a percentage. It is agreeing on what the line was scheduled to make, where bags are counted, and which events change each figure.
Why Two Teams Can Report Different OEE for the Same Shift
One supervisor removes changeovers from planned production time. Another includes them as availability loss. The HMI counts every cut piece, while quality counts only packed bags. Startup waste goes into a recycling bin and disappears from the report. A five-minute material shortage is recorded as maintenance because the machine was stopped. Both teams can calculate a neat percentage, but neither number can be audited.
ISO 22400-2 defines manufacturing-operations KPIs and describes formulas, elements, units, and time behavior. It does not choose one commercial policy for every factory. A plant must still publish its own data dictionary and apply it consistently.
Define the Measurement Boundary Before the Formula
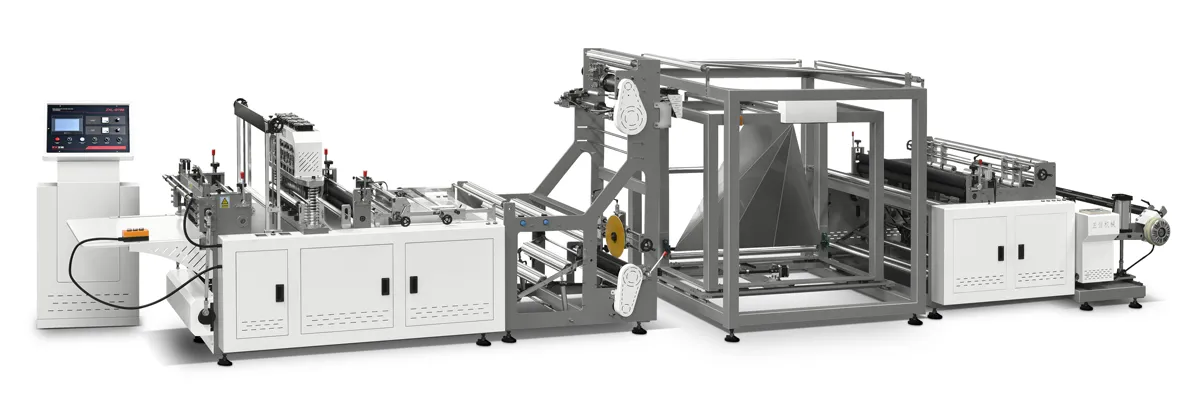
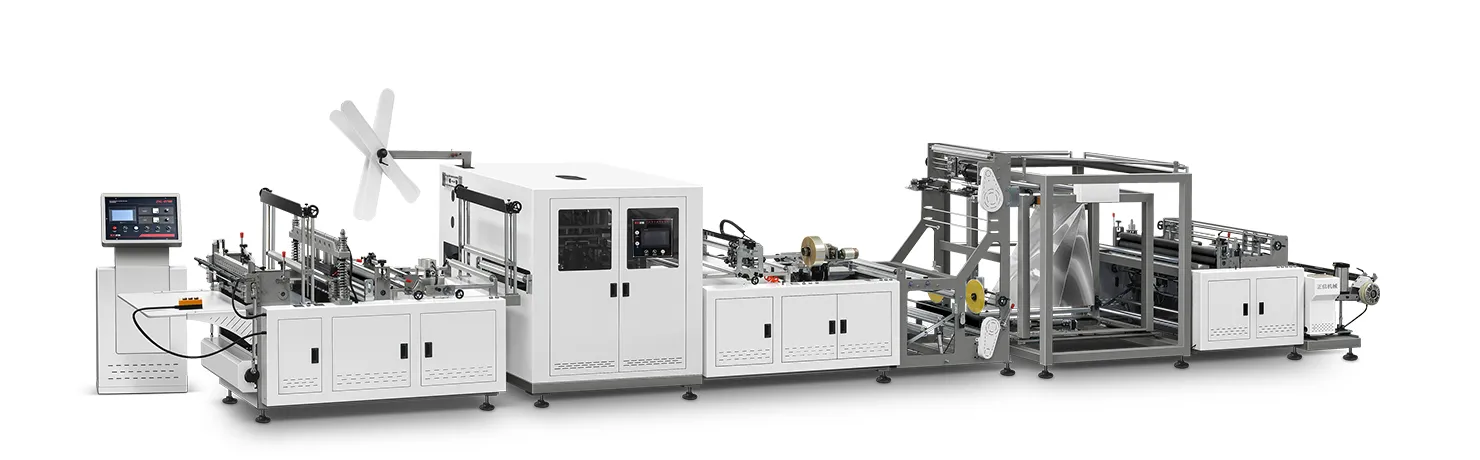
Choose the work unit first. It may be the bag-making machine alone or the complete line from roll feed to accepted stack. Do not switch boundaries between shifts. If an offline punch or handle station limits shipments, machine-only OEE can look healthy while orders remain late.
| Field | Definition to freeze | Evidence source |
|---|---|---|
| Planned production time | Scheduled interval after named exclusions | Approved shift and order schedule |
| Run time | Planned time minus recorded stop time | PLC state history plus operator reason |
| Ideal cycle time | Validated time per bag for one named product | Approved recipe or capability trial |
| Total count | All units crossing one physical count point | Counter reconciliation |
| Good count | Units accepted at the same boundary | Quality and packing record |
Bag style, size, fabric, print registration, handle process, and pack count belong in the record. A mixed shift should not use one ideal cycle time unless the calculation is weighted by the actual product periods.
Use the Three Factors Without Hiding Their Inputs
The common structure is:
- Availability = Run Time ÷ Planned Production Time
- Performance = Ideal Cycle Time × Total Count ÷ Run Time
- Quality = Good Count ÷ Total Count
- OEE = Availability × Performance × Quality
Keep units consistent. If run time is in minutes and ideal cycle time is seconds per bag, convert one before calculating. An OEE result above 100% usually indicates a wrong ideal cycle time, mixed boundaries, duplicated counts, or a unit error.
Consider an illustrative shift with 420 planned minutes, 45 minutes of stops, an approved ideal cycle of 0.60 seconds per bag, 32,000 total bags, and 30,720 good bags. Availability is 89.3%, performance is 85.3%, quality is 96.0%, and OEE is about 73.1%. These figures demonstrate the calculation only; they are not Zhengxin performance promises or industry targets.
Count Good Output Where the Customer Requirement Is Complete
The most useful production number is often good bags per scheduled hour, not OEE alone. A bag should not become good merely because it passed the cutter. If the order requires an attached handle, registered print, a specified stack count, or an offline operation, the acceptance point must include that condition.
Reconcile three counts at the end of every job:
- Input or theoretical pieces based on consumed web length.
- Machine total count at the defined sensor.
- Accepted packed quantity plus classified rejects and work in process.
A gap is a data problem. Do not distribute it automatically across known scrap categories.
Build a Loss Tree That Operators Can Actually Use
Ten clear stop reasons are better than fifty overlapping codes. Record the symptom first, then investigate cause. An operator may know that the web wandered or the handle feed stopped; the later root-cause review may find material winding, a sensor, air pressure, or setup error.
| Loss family | Example observable event | Do not confuse with |
|---|---|---|
| Equipment stop | Drive alarm or ultrasonic trip | Planned tool change |
| Setup and adjustment | Bag-size or tooling change | Unrecorded startup production |
| Material delay | No approved roll at the line | Machine feed fault |
| Small stop | Short jam or stack correction | Reduced steady speed |
| Process defect | Weak seam during stable run | Startup trial waste |
| Reduced yield | Rejected bags before stable output | Accepted setup samples |
Use a threshold that the plant can collect reliably, and keep it unchanged long enough to compare periods.
Audit the Data Before Improving the Machine
For one representative order, compare PLC events, HMI counts, roll usage, quality sheets, packing records, and the operator log. Watch the line clock for a short period. Look for missing micro-stops, simultaneous reason codes, counts that continue during reject production, and manual edits without a trace.
Then rank loss in minutes and lost good bags. Do not start with the largest percentage on a dashboard. A recurring 20-second stack correction may consume more capacity than one dramatic breakdown. A low quality factor may come from a measurement or material issue rather than machine speed.
What to Send a Machine Supplier for a Useful Review
A Manufacturer cannot diagnose a percentage. Send the machine model and serial number, bag drawing, fabric specification, approved recipe, shift timeline, alarm export, total and good counts, scrap categories, sample photos, and the exact calculation policy. A Supplier can then separate machine, material, method, and measurement questions.
Zhengxin can review this evidence against the delivered OEM or Customizable line configuration and help define a focused trial. The expected output is a test plan and a short list of verified loss mechanisms, not a generic promise to raise OEE.
 አማርኛ
 English
 العربية
 Español
 Русский
 O‘zbekcha
 Қазақ тілі
 Português (AO90)
 Tiếng Việt
 (فارسی (افغانستان
 Kiswahili
 தமிழ்
 Bahasa Indonesia
 اردو
 हिन्दी
 বাংলা